Why Plastic Packaging Barrier Properties Matter
When food manufacturers and nutraceutical brand owners develop new products, they often focus on formulas, flavors, and nutrition ratios. However, packaging barrier performance is one of the most overlooked but decisive factors that determine a product’s shelf life, market reputation, and shelf stability.
Many failed retail cases happen not because of poor product formulas, but because of improper plastic packaging selection. Moisture ingress, oxygen oxidation, and light damage will gradually ruin protein powder, gummies, snacks, and nutritional supplements during transportation and shelf display.
What Are Packaging Barrier Properties?
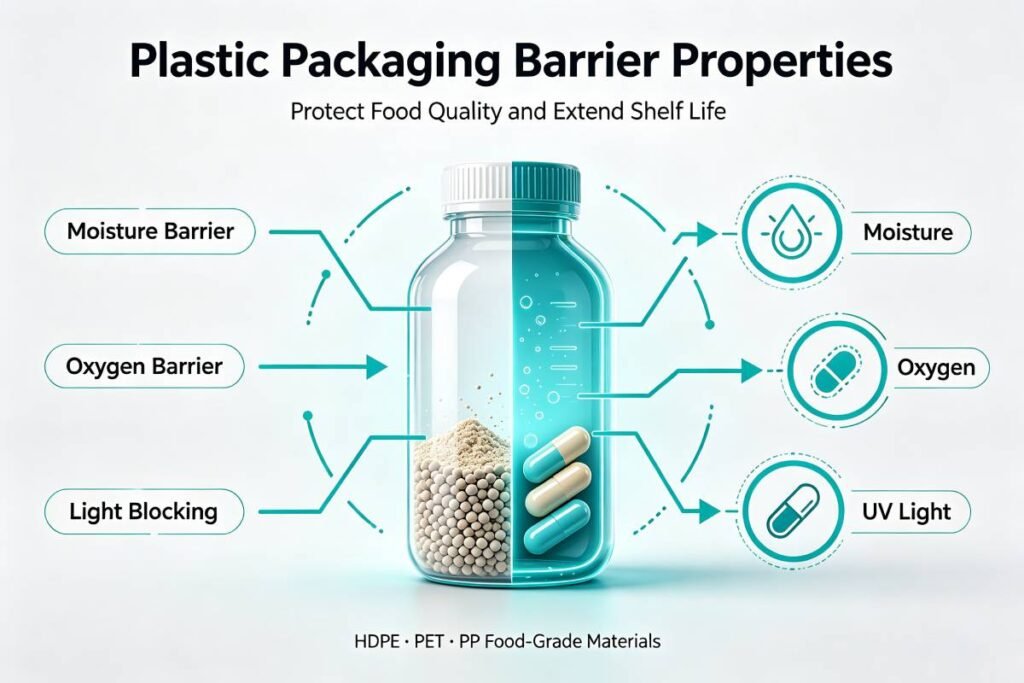
Barrier properties refer to a plastic container’s ability to block moisture, oxygen, UV light, and dust. Different food-grade plastic materials deliver completely different barrier results:
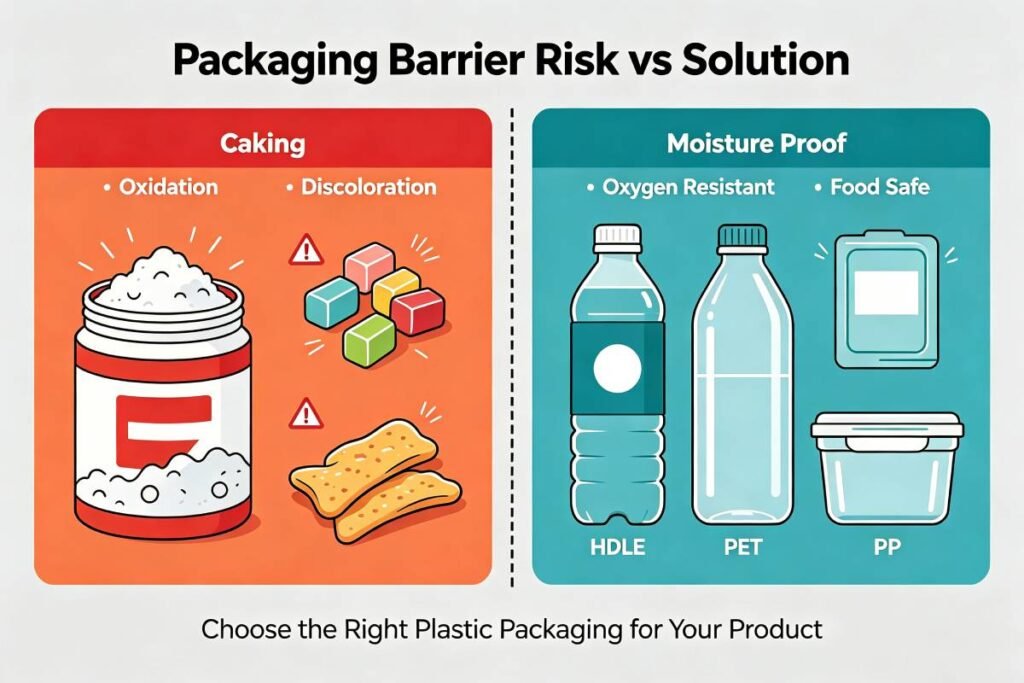
HDPE plastic: Excellent moisture-proof and light-blocking barrier. It is the best choice for protein powder, meal replacement powder, and dry nutraceutical products that require long shelf life.
PET plastic: Clear and transparent with moderate oxygen barrier performance. Ideal for displaying gummies, candies, and snack products that require retail visual appeal.
PP plastic: Stable chemical barrier and high-temperature resistance, suitable for sauce packaging and hot-filled food products.
Without matching barrier performance, even high-quality food and supplement formulas will face caking, discoloration, oxidation, and short expiration time.
How Poor Barrier Packaging Hurts Your Products
1. Moisture penetration causes caking
Protein powder and dietary supplements easily absorb moisture in the air. Low-barrier plastic jars lead to hard lumps, affecting customer experience and product sales.
2. Oxygen oxidation damages nutrition
Vitamins, probiotics, and organic nutrition ingredients are sensitive to oxygen. Poor barrier packaging accelerates nutrition loss.
3. Light exposure degrades product quality
Bright light destroys active ingredients in supplements. Opaque HDPE packaging effectively solves this problem.
4. Shorter shelf life increases return rates
Retailers and supermarket chains strictly require long shelf life. Unqualified barrier packaging makes products difficult to enter mainstream sales channels.
How to Choose the Right Barrier Packaging for Your Products
Protein powder & dry supplements: Choose thickened HDPE food-grade jars for maximum moisture and light barrier.
Gummy & candy snacks: Use transparent PET bottles for display while ensuring basic oxidation resistance.
Sauce & wet food: Adopt high-temperature resistant PP bottles with good chemical stability.
Export EU & US market: Select FDA and EU compliant food-grade packaging produced in a clean workshop to ensure stable barrier safety.
Brotherpack Barrier Packaging Advantages
As a professional food-grade plastic packaging manufacturer, Brotherpack customizes barrier solutions according to different product characteristics.
All plastic jars and bottles are produced in a 100,000-class clean workshop, using pure food-grade PET, HDPE, and PP raw materials. We provide customized thickness, opaque/transparent design, child-resistant caps, and sealing solutions to enhance barrier performance.
Professional barrier packaging design directly extends your food and supplement shelf life, reduces after-sales problems, and improves brand competitiveness in global wholesale markets.
More videos for your Learning in our youtube channel
FAQ
Q: Which plastic material has the best moisture barrier for protein powder?
A: HDPE food-grade plastic provides the strongest moisture-proof and light barrier, which is the most widely recognized packaging material for protein powder and dry nutritional supplements.
Q: Can transparent PET bottles protect snack food from oxidation?
A: Yes. Standard food-grade PET containers offer basic oxygen barrier performance, perfect for short-to-medium shelf life snack and gummy products.
Q: Does clean workshop production improve packaging barrier stability?
A: Absolutely. Dust-free clean workshop production avoids impurities inside plastic materials, ensuring stable barrier performance and food safety for export markets.
Q: Can you customize high-barrier packaging for special nutrition products?
A: Yes. Brotherpack supports customized bottle thickness, material formulas, and sealing processes to upgrade barrier performance for high-standard food and nutraceutical products.